Inline Integration: Horizontal Cartoner to 3D Overwrapper & Case Packer
Integrate 3D cellophane overwrapping machines downstream of horizontal cartoners, checkweighers, 2D serialization cameras, and multi-pack bundlers.
Turning Standalone Overwrappers into Synchronized Secondary Lines
In automated cosmetic, tea, and pharmaceutical plants, a cellophane wrapping machine sits directly between the horizontal cartoner/checkweigher and the final case packer or bundle wrapper. Mechanical orientation transfers (90° turning guides or starwheels), backlog photoeyes, and dry-contact PLC interlocks determine whether cartons flow smoothly at 80–150 BPM or jam at the infeed gate.
We engineer complete secondary transfer conveyors, bypass lanes for unwrapped export SKUs, and post-wrap vision verification.
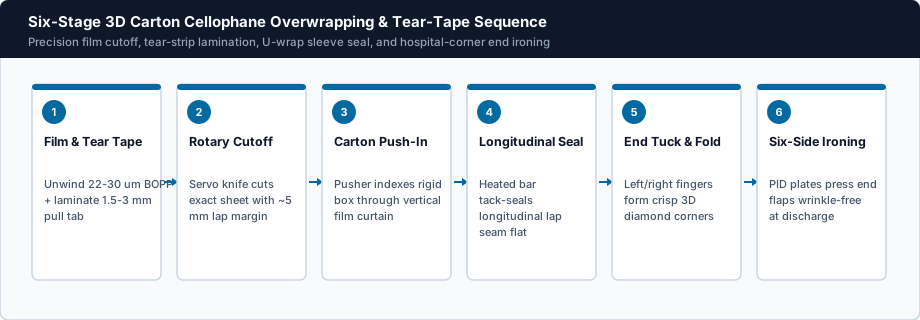
Secondary Cartoning-to-Overwrapping Interface Architecture
Key station handshakes from primary carton closing to master case loading:
| Upstream / Downstream Link | Mechanical Transfer Hardware | Control & Inspection Interlock | Speed Margin Rule |
|---|---|---|---|
| 1. Cartoner Discharge | Side-belt transfer + 90° orientation turner | Open-flap reject prior to overwrapper | 100% base line rate |
| 2. Checkweigher + Serialization | Stabilized Vacuum belt + 2D camera | Reject missing-leaflet/bad-code cartons first | Prevents wrapping defective packs |
| 3. Buffer & Overwrapper Infeed | 1.5–3.0 m low-friction accumulation belt | Low/high backlog photoeyes modulate speed | Overwrapper rated 115–120% of cartoner |
| 4. Bundle / Case Packer Outfeed | Cooling belt + stacker collator | Downstream full sensor pauses pusher cleanly | Zero carton-stop-on-heater scorching |
Review machine platforms in automatic box overwrappers and factory capability on cellophane wrapping machine manufacturer.
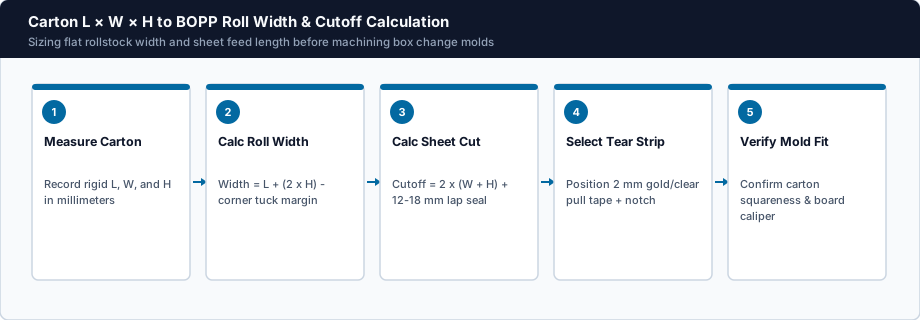
3D Overwrapping Engineering Notes
- Clear-Heater Auto-Retract: If downstream case packing pauses, pneumatic retractors pull PID heater plates 10 mm back from stationary cartons so BOPP never melts through.
- Bypass Conveyor Option: Install a diverter gate when certain domestic SKUs ship unwrapped while export/duty-free SKUs require 3D tear-tape overwrapping.
- Print-and-Verify After Wrap: Apply shipping vignette labels or verify GS1 codes through optical-clarity BOPP without glare using polarized LED ring lights.
Request a Secondary Line Layout Drawing
Share your upstream cartoner model, discharge height (typically 800–900 mm), and carton orientation via our Project Brief.
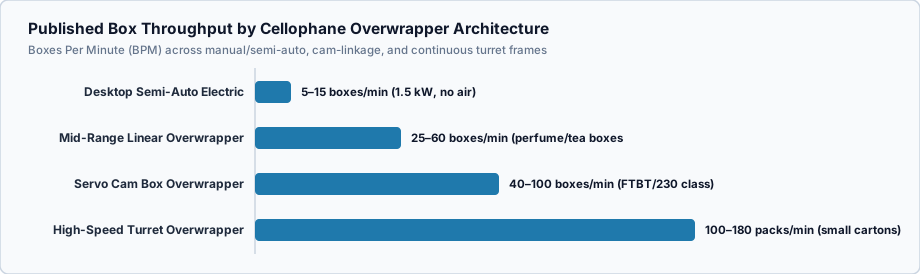
Explore related systems in Cellophane Wrapping Machines, BOPP & Cellophane Film Specs, or submit your carton L×W×H via Project Brief.
Further Reference
Verify Dimensions & Operating Ratings
Send your target envelope, load requirements, and ambient environment to review matching configurations.